If you’ve ever stood in a busy automotive assembly plant, watching a car chassis roll steadily from a welding station to a paint booth, or observed a bottling line where plastic bottles glide seamlessly from rinsing to labeling to capping, you’ve likely seen curved conveyor chains at work. As a conveyor chain supplier, I field questions about these specialized components almost daily, and most people are surprised to learn just how far their applications stretch beyond basic assembly lines. Curved conveyor chains aren’t just another piece of industrial hardware—they’re engineered solutions that solve specific spatial and performance challenges that straight conveyors can’t address. Today, I want to break down their most impactful uses, share real-world examples from clients I’ve worked with, and explain why partnering with the right supplier matters when you’re integrating these chains into your operation. Conveyor Chain

First, let’s start with the basics for anyone new to the space: curved conveyor chains are not your standard straight-link conveyor chains. They’re designed with precise side-flexing capabilities, meaning they can navigate tight horizontal turns (from 15-degree increments to full 180-degree U-shaped loops) without binding, jamming, or losing load stability. Unlike belt conveyors, which can slip or warp when forced around sharp corners, these chains transfer heavy or bulky loads evenly, thanks to their interlocking link design and load-bearing attachments called flights, pallets, or buckets. That flexibility is what makes them indispensable in facilities where floor space is a premium, or where production lines need to loop, merge, or split paths without disrupting workflow.
One of the most common applications I see is in automotive and heavy equipment manufacturing. My team has supplied curved chains to several domestic and international auto assembly plants over the past decade, and their use here is game-changing. Take the final assembly line, for example: a typical plant needs to route fully assembled vehicles through a sequence of quality checks, wheel installation, battery connection, and final packaging. A straight conveyor would require a 200-foot straight stretch to turn a line 180 degrees, which takes up valuable floor space that many plants can’t spare. Curved conveyor chains, by contrast, can make that same 180-degree turn in as little as 10 feet, letting plants compact their lines and reallocate that space to add workstations or storage. One client in Michigan told me that after switching to curved chains for their body shop line, they reduced their line footprint by 35% in one area and added two extra painting bays without any construction of new facilities. That kind of efficiency is exactly why automotive manufacturers rely on these chains so heavily—they also handle uneven loads, like unfinished truck chassis, better than alternative conveyors, thanks to their high load capacity (many of our heavy-duty curved chains can carry up to 10,000 pounds per link).
Next, the food and beverage industry is another massive user of curved conveyor chains, and for good reason. This sector has non-negotiable requirements: hygiene, speed, and consistent flow. Curved chains for food applications are made from food-grade stainless steel or FDA-approved plastic composites, so they’re safe for contact with food products like bottled soda, fresh produce, baked goods, or canned goods. The side-flexing design is perfect here because bottling lines often need to merge multiple lines of bottles into one, or split a single line into two for different packaging sizes—something straight conveyors can’t do without complex transfer mechanisms. Last year, a craft brewery in Ohio reached out to me because their old straight line was causing delays when switching between 12-oz cans and 16-oz growlers. We supplied them with curved plastic conveyor chains that let their line loop and split seamlessly, cutting changeover time by 22% and reducing bottle jams by 80%. Another client in the fresh produce industry uses curved stainless steel chains to route bulk apples and berries from washing stations to sorting and packaging areas, navigating tight corners to fit the line into their climate-controlled warehouse without cross-contamination risks. Food-grade curved chains also are easy to clean—they have fewer crevices than roller belt systems, so they meet strict food safety regulations without extra downtime for sanitizing.
Beyond manufacturing and food, curved conveyor chains are critical in material handling and logistics, especially in distribution centers and parcel hubs. E-commerce growth has put pressure on these facilities to process thousands of packages an hour, and space is always tight. Curved chains are used in sortation systems, where packages of all shapes and sizes need to be routed to different chutes based on their destination. For example, a 180-degree curved conveyor chain can move a small package from the main sorting line to a loading dock in a fraction of the space a straight conveyor would need. I worked with a major parcel provider in Texas that expanded their sortation line last year, and instead of laying 1,000 extra feet of straight conveyor, they used 300 feet of curved chain loops. That cut their installation time by 40% and reduced energy use—curved chains have less friction when turning, so they require less horsepower to operate than straight conveyors pushing loads around large corners. They also handle irregular-shaped loads, like large boxes or furniture, better than belt conveyors, which can slip or shift heavy items mid-turn. Another logistics client uses curved chains to build temporary storage loops for overflow packages during peak holiday seasons, letting them double their capacity without investing in permanent structural changes.
A less talked about but equally important application is in the pharmaceutical and medical device industry. This sector demands precision, cleanliness, and compliance with strict regulations like GMP (Good Manufacturing Practices). Curved chains here are typically made from high-grade stainless steel or medical-grade plastic, with no crevices or rough edges that could trap bacteria or debris. They’re used to transport delicate products like syringes, vials, and implantable medical devices, where even a tiny jolt or jam could damage the product. The smooth, consistent movement of curved conveyor chains ensures that fragile items stay stable around corners, and many of our clients in pharma use custom attachments (like low-profile pallets or soft rubber flighting) to secure delicate loads without scratching them. One client in Ireland that produces insulin pens told me that before switching to our curved chains, they were experiencing a 1.2% defect rate from jams on their vial line. After we installed our precision-machined curved chains, that defect rate dropped to 0.02%, saving them hundreds of thousands of dollars in product losses annually. Curved chains also work well in cleanroom environments—their sealed design prevents lubricants from leaking onto products, which is a non-negotiable requirement for many medical manufacturing facilities.
Now, I want to be clear: curved conveyor chains aren’t one-size-fits-all, and that’s where a reliable supplier makes all the difference. I’ve worked with clients who tried to save money by buying generic curved chains from a non-specialized supplier, only to face constant jams, increased maintenance, and even product damage within six months. The best curved conveyor chains are engineered with precise link pitches, flexural point reinforcement, and load testing tailored to your specific application. For example, a curved chain for a bottling line needs different flex capabilities than one for an automotive assembly line—botting lines require tight 15-degree turns at high speed, while heavy automotive lines need wider turns and higher load capacity. As a conveyor chain supplier, I don’t just sell products; I work with clients to assess their space constraints, load requirements, speed needs, and regulatory compliance needs to design a custom solution. We offer both standard and custom curved chains, with options for stainless steel, plastic, or carbon steel, and we provide ongoing maintenance support to ensure the chains operate at peak performance for years.
If you’re thinking about integrating curved conveyor chains into your operation, here are a few key considerations to keep in mind. First, measure your available floor space accurately—curved chains can reduce footprint, but you need to account for the required clearance around the turns (we can help with that during the design phase). Second, know your load specifications: how much does each load weigh, what’s the shape of the load, and is it uneven? Third, consider your operating environment: is it a food-grade facility, a cleanroom, or a heavy industrial plant? All of these factors will determine the right material and chain design. Finally, partner with a supplier that has experience in your industry—someone who can provide references from other clients in the same sector, and who offers support beyond just the initial purchase.
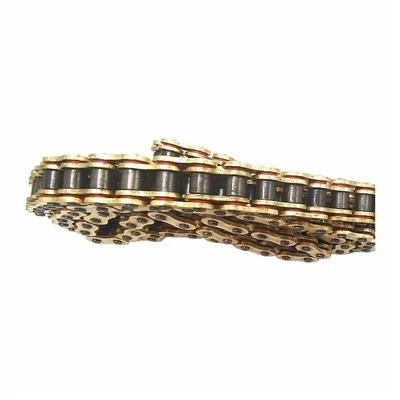
At the end of the day, curved conveyor chains are a quiet workhorse in many of the industries that keep our economy running. They let manufacturers produce goods faster, safer, and more efficiently, while reducing operational costs and space constraints. If you’re looking to upgrade your production line, reduce bottlenecks, or save floor space, curved conveyor chains might be the solution you’ve been overlooking. If you’d like to discuss your specific needs, our team is here to help you find the right chain for your application. We can walk you through design options, provide performance data, and answer any questions you have about integrating curved chains into your operation. Don’t let outdated straight conveyors limit your efficiency—reach out today to start a conversation about how curved conveyor chains can transform your workflow.
Driving Chain References:
- Conveyor Equipment Manufacturers Association (CEMA). Conveyor Equipment Design Standards for Industrial Applications, 2021.
- Food and Drug Administration (FDA). Guidance for Industry: Manufacturing Equipment and Utensils for Food Contact Surfaces, 2020.
- Pharmaceutical and Medical Devices Association (PMDA). GMP Compliance Guidelines for Conveyance Systems in Drug Manufacturing, 2022.
- Logistics Management Institute. Space Optimization in Distribution Centers: The Role of Curved Conveyors, 2021.
Anhui Huihuang Chain Transmission Co., Ltd.
Anhui Huihuang Chain Transmission Co., Ltd. is one of the most professional conveyor chain manufacturers and suppliers in China, also supports high quality customized service. Please feel free to buy discount conveyor chain made in China here from our factory. Welcome to contact us for pricelist and free sample.
Address: NO.3 YONGQIANG ROAD. JIXI.ANHUI.CHINA
E-mail: 754590660@qq.com
WebSite: https://www.hhchains.com/
